Blog
Blog
Blog
2026 Best EVA Shoe Mould Manufacturers for Global Buyers
Choosing the right EVA Shoe Mould manufacturer can shape product quality, production speed, and long-term business stability. In 2026, global buyers face a crowded supplier market. Many factories present attractive prices, yet price alone cannot confirm mould performance. Practical evaluation matters more.
A reliable manufacturer should understand EVA foaming behavior, mould structure, temperature control, and dimensional accuracy. Buyers should review machining capabilities, material selection, sample approval, and quality inspection records. Clear communication also matters when drawings, sizes, logos, or regional standards change. A factory visit is useful, but detailed video inspections can provide valuable evidence when travel is difficult. Ask for actual samples. Examine the sole pattern, edges, vents, surface finish, and alignment under production conditions.
This guide compares leading manufacturers through an international buyer’s perspective. It considers technical expertise, customization capacity, delivery reliability, after-sales support, and documented manufacturing experience. Certifications can help, but they should not replace direct verification. A polished website proves little.
No supplier is flawless. Even experienced mould makers may face delays, trial adjustments, or uneven communication across time zones. That weakness deserves honest attention. Buyers should confirm revision policies, replacement terms, testing procedures, and total landed costs before signing an order. Small details often become expensive problems later.
The manufacturers discussed here are selected for their practical capabilities and suitability for global footwear projects. The ranking is not absolute. Your production volume, target market, EVA formula, and design complexity may change the best choice. Use this overview as a focused starting point, then validate every important claim with samples, records, and direct discussion.
What Makes an EVA Shoe Mould Manufacturer a Top Global Choice in 2026
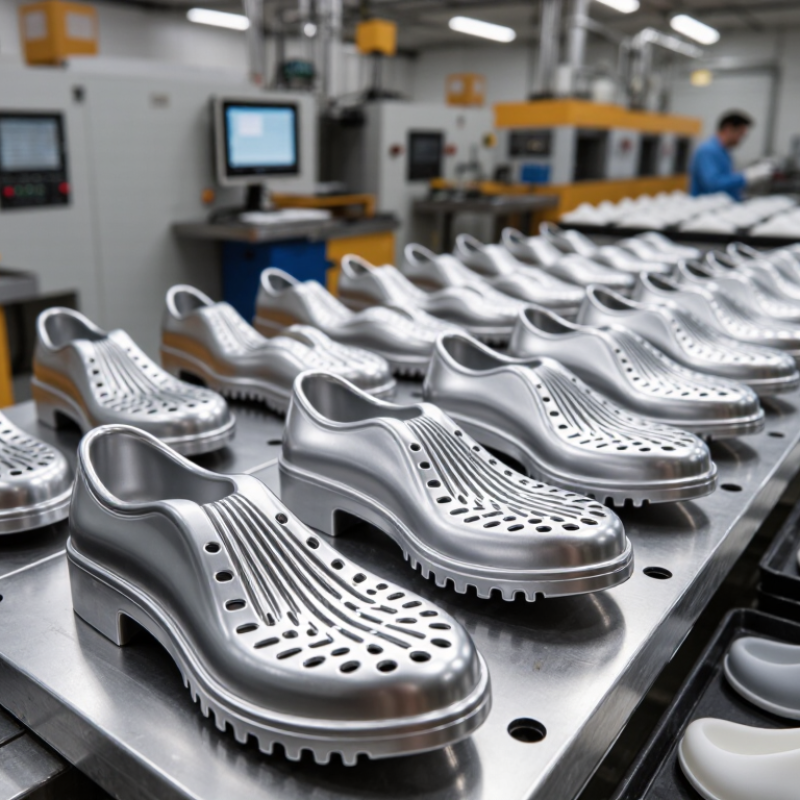
In 2026, a top EVA shoe mould manufacturer must do more than cut steel accurately. Global buyers need predictable mould performance, clear technical advice, and evidence from repeated production runs. Experienced teams study the outsole drawing, foam behavior, shrinkage, and expected cycle time before recommending a mould structure. They should ask uncomfortable questions about fit, texture, drainage, and repair access. Small details matter. A one-millimeter error can change comfort and material balance.
Professional capability appears in the process. Engineers should use reliable CAD data, controlled machining, trial samples, and documented inspections. Buyers should receive dimensional reports, material information, and realistic delivery schedules. A strong manufacturer also understands different factory conditions. Temperature, injection pressure, and operator habits can affect EVA results. Remote support helps, but clear video records and measured feedback work better than vague promises. Communication must survive time zones and language differences.
Authority is built through traceable experience, not polished claims. Ask for relevant case evidence, sample approval records, and references where appropriate. Quality systems should cover incoming materials, tool wear, surface finish, and final checks. Compliance knowledge also matters when moulds cross borders. No manufacturer is flawless. Even skilled teams may miss a change in foam formulation or overlook a difficult texture. The best partners admit the risk, propose a correction, and record the lesson. That honesty often protects a global project more than a perfect sales presentation.
Key Types of EVA Shoe Moulds and Their Manufacturing Applications
Compression EVA shoe molds remain widely used for midsoles, sandals, slippers, and casual soles. They shape pre-expanded EVA sheets under heat and pressure. This method supports different densities, textured bottoms, and practical production volumes. Mold cavities need balanced heating and accurate venting. Otherwise, trapped air can leave marks near the heel.
Injection EVA molds suit automated production and high-volume footwear lines. They feed expanded EVA material directly into controlled cavities. This process helps create consistent thickness, curved sidewalls, and lightweight sports midsoles. Designers can add separate zones for heel support or forefoot flexibility. Cooling channels also matter. Poor cooling may cause shrinkage, uneven edges, or delayed demolding.
Two-color and multi-density molds support sandals, fashion soles, and performance footwear with contrasting sections. Some factories use aluminum for faster heat transfer and steel inserts for repeated wear areas. Buyers should inspect cavity tolerances, surface finish, vent placement, and trial samples before approving a mold. A useful test checks weight, rebound, dimensions, and sole bonding after several production cycles. The first trial is rarely perfect. Small changes in pressure, temperature, or expansion time can improve the result. Still, over-correction may damage surface detail. Experienced mold engineers record each adjustment and compare samples under consistent conditions. That record provides stronger evidence than attractive drawings or promises.
2026 Best EVA Shoe Mould Manufacturers for Global Buyers - Key Types of EVA Shoe Moulds and Their Manufacturing Applications
| EVA Shoe Mould Type | Primary Manufacturing Application | Typical Tool Material | Typical EVA Process | Best-Fit Product | Key Buyer Evaluation Criteria |
|---|---|---|---|---|---|
| Compression Mould | Moulding expanded EVA sheets or preforms into midsoles, outsoles, sandals and lightweight footwear components. | Aluminium alloy is widely used for production tooling because it combines machinability, thermal conductivity and moderate weight. | Heat, compression and cooling in a matched cavity; cycle settings depend on EVA formulation, density and part thickness. | Athletic midsoles, casual soles, slippers and general-purpose EVA footwear. | Cavity balance, venting, shrinkage allowance, cooling-channel layout, surface finish and repeatability between cavities. |
| Injection EVA Mould | High-volume production of directly injected EVA soles and integrated footwear parts. | Aluminium or tool steel, selected according to production volume, pressure, wear requirements and machine compatibility. | EVA pellets or granules are plasticized and injected into a heated mould before curing, expansion and cooling. | Direct-injection sandals, sports soles, comfort footwear and moulded one-piece components. | Gate position, runner design, flash control, filling uniformity, venting, demoulding angle and machine interface. |
| Two-Color or Multi-Color Mould | Production of soles with contrasting colors, dual-density zones, decorative patterns or functional traction areas. | Machined aluminium for many applications; wear-resistant steel inserts may be added at high-wear locations. | Sequential compression or injection cycles with controlled material placement and interlayer bonding. | Lifestyle soles, children's footwear, fashion sandals and performance designs with separate cushioning zones. | Color registration, bonding between layers, shut-off accuracy, cavity alignment, material compatibility and cleaning access. |
| Dual-Density Mould | Combines softer cushioning EVA with a firmer support or wear layer in one sole structure. | Aluminium cavities with replaceable steel or hardened inserts where compression, abrasion or sharp details are concentrated. | Two-stage moulding, insert moulding or sequential material placement, depending on the construction and equipment. | Running shoes, walking shoes, work-inspired casual footwear and comfort products requiring support zoning. | Interface strength, density separation, material-flow control, compression-set behavior and dimensional stability after cooling. |
| Microcellular EVA Mould | Manufacturing fine-cell foam components with a balance of low weight, resilience and cushioning. | Aluminium or steel, with carefully finished cavity surfaces and controlled venting features. | Foam expansion and cross-linking under controlled temperature, pressure and curing time. | Lightweight midsoles, insoles, comfort sandals and cushioning inserts. | Cell uniformity, density distribution, expansion allowance, vent design, shrinkage control and compression-set performance. |
| Textured Outsole Mould | Creates lugs, grooves, ribs, logos, geometric textures and other traction features on EVA outsoles. | Aluminium for standard patterns; steel inserts or hardened surfaces for deep, narrow or high-wear details. | Compression or injection moulding with cavity engraving, CNC machining, EDM or chemical/textured finishing as required. | Outdoor sandals, casual soles, indoor footwear and products requiring improved grip or visual definition. | Texture depth, edge sharpness, draft angle, flash removal, slip-resistance design intent and ease of cleaning. |
| Prototype or Development Mould | Fast validation of sole geometry, fit, tooling concept, material behavior and design details before production tooling. | Aluminium, soft tooling materials or additively manufactured patterns, depending on the required process and number of trials. | CNC machining, additive pattern production, low-volume compression or trial injection. | New footwear concepts, seasonal collections, fit samples and engineering verification units. | Speed of design changes, sample accuracy, data compatibility, revision control, repairability and conversion to production tooling. |
| Replaceable-Insert Mould | Supports interchangeable sizes, sole patterns, logos, tread blocks or high-wear cavity sections. | Aluminium base with steel, stainless steel or hardened inserts selected for durability and dimensional retention. | Compression or injection moulding using mechanically located and secured inserts. | Multi-size footwear ranges, seasonal design updates and products with frequently revised tread features. | Insert repeatability, locating accuracy, sealing against flash, replacement time, spare-part availability and maintenance access. |
| Full-Shoe or Slipper Mould | Forms larger three-dimensional EVA products, including full-foot slippers, clogs and integrated upper-sole designs. | Aluminium is common for production cavities; steel may be used for areas needing greater wear resistance. | Compression, injection or expanded-foam moulding, depending on the product construction. | Slippers, clogs, house shoes, children's footwear and molded comfort footwear. | Last geometry, wall-thickness consistency, demoulding strategy, foot-opening accuracy, ventilation and surface quality. |
| Logo and Decorative-Detail Mould | Produces recessed or raised lettering, symbols, branding-free graphics, decorative grooves and visual identifiers. | Aluminium, steel inserts or copper electrodes for detailed EDM work, depending on feature depth and resolution. | CNC engraving, laser marking, EDM and precision finishing integrated into compression or injection tooling. | Fashion soles, promotional footwear, private-label products and designs requiring clear visual details. | Letter legibility, minimum feature size, cavity cleanliness, draft angle, alignment and resistance to wear during repeated cycles. |
Global Buyer Specification Checklist for EVA Shoe Moulds
| Evaluation Dimension | Typical Requirement or Industry Practice | Why It Matters |
|---|---|---|
| CAD and Data Compatibility | Confirm accepted 3D formats such as STEP, IGES or native CAD files, together with a controlled revision process. | Reduces geometry errors and ensures that the approved sample matches the production tool. |
| Dimensional Control | Agree on datum points, inspection method, cavity-to-cavity matching and allowance for EVA shrinkage and expansion. | EVA parts can change dimensions during heating, foaming, cooling and post-mould conditioning. |
| Venting and Flash Control | Review vent locations, parting lines, shut-offs and trimming requirements during the design stage. | Proper venting helps reduce trapped air, incomplete filling, surface defects and excessive flash. |
| Thermal Management | Check heating uniformity, cooling-channel design, temperature monitoring and compatibility with the intended moulding machine. | Uneven temperature distribution can cause inconsistent density, shrinkage, color and surface appearance. |
| Surface Finish | Specify polished, matte, textured, engraved or chemically treated surfaces according to the approved sample. | Cavity finish directly influences the appearance, release behavior and cleanability of the EVA component. |
| Quality Documentation | Request approved drawings, material certificates, inspection records, trial reports, maintenance instructions and spare-part lists. | Complete documentation supports repeat orders, troubleshooting, audits and tool transfer between factories. |
| Performance Testing | Evaluate finished EVA parts for density, hardness, compression set, abrasion, dimensional stability and slip-related requirements where applicable. | Tool quality must be verified through finished-part performance rather than appearance alone. |
| Maintenance and Serviceability | Confirm cleaning procedures, insert replacement, vent maintenance, corrosion protection and access to technical support. | Regular maintenance preserves cavity accuracy, reduces flash and extends useful tooling life. |
How to Evaluate EVA Shoe Mould Quality, Technology, and Customization
When evaluating EVA shoe moulds, buyers should inspect more than polished steel. The World Footwear Yearbook 2024 recorded about 23.9 billion pairs produced globally in 2023. That scale makes repeatability essential. A reliable mould should hold cavity dimensions, vent evenly, and release cleanly after every cycle. Ask for CMM inspection records, steel-grade details, and trial-shot measurements. Check the outsole’s heel, arch, and toe areas separately. Small errors often appear there first.
Material performance needs practical testing. ASTM D3575 provides methods for evaluating flexible cellular materials, including density and compression-related properties. Compare mould samples by weight, rebound, hardness, and compression set. A stable mould should support consistent EVA expansion, not merely create a sharp-looking prototype. Watch the foam around vents and deep grooves. Burn marks, uneven cell structure, or flashing may indicate poor air evacuation or incorrect processing settings. The mould may not be the only problem.
Customization begins with the last, not the artwork. Confirm shrinkage compensation, wall thickness, draft angles, logo depth, and cooling-channel layout before machining. CAD files should be checked against a physical last. Digital accuracy can still miss a real fitting issue. Request at least one pilot run and retain measured samples for comparison. In my experience, suppliers sometimes promise tight tolerances without defining the measurement point. That deserves a second question. A strong technical partner explains limitations clearly and records every revision.
Global Compliance, Production Capacity, and Export Service Standards
2026 Best EVA Shoe Mould Manufacturers for Global Buyers
Global Compliance, Production Capacity, and Export Service Standards
Reliable EVA shoe mould manufacturers treat compliance as part of production, not paperwork added later. Buyers should request material declarations, chemical test reports, and traceable quality records. Requirements differ across markets, so factories must review applicable product safety, labeling, and environmental rules. Clear documentation reduces customs delays and protects long-term supply relationships. Records matter.
Production capacity needs practical verification. A supplier may state a large monthly output, but available machine hours tell a better story. Ask about moulding equipment, shift patterns, cavity numbers, and backup capacity. Review sample schedules and recent delivery performance. A factory producing 20,000 pairs daily may still struggle with customized orders. Capacity figures can look impressive. They need context.
Export service should include stable packaging, accurate invoices, and responsive technical support. Experienced teams confirm mould drawings before machining and record approval changes carefully. They should also explain lead times for sampling, revisions, production, and replacement parts. In practice, communication is not always perfect. Language gaps or late confirmations can create costly errors. A shared specification sheet helps both sides. Check how the manufacturer handles damaged cargo, inspection findings, and urgent corrections. Honest reporting is more valuable than optimistic promises.